Views: 0 Author: Site Editor Publish Time: 2026-09-04 Origin: Site


Today, shoppers are more committed than ever to packaging that’s kinder to the planet. Across every store aisle, plastic is being swapped out for greener alternatives. If you’re struggling to find a supplier that keeps food safe, holds up through transit, and stays eco-friendly, you’re not alone. This guide highlights the top 10 food packaging tube suppliers for 2026, focusing exclusively on companies based in Europe and America. You’ll also get a practical supplier evaluation framework to help you make a confident, informed decision. Keep an eye out for a special spotlight on hallpack, a leading OEM/ODM partner with over 20 years of industry expertise. Whether you’re searching for the best cardboard tube manufacturer or top-rated suppliers for specialty paper tubes used in food packaging, this guide covers all your options. Paper tube manufacturers offer a wide range of solutions, but truly sustainable packaging demands careful evaluation—and we’re here to help you navigate it.
Make sure the supplier has FDA or EU approval before you pick them.
Pick PE coating to resist moisture, or pick PLA to be compostable.
Look at each supplier’s minimum order size, how fast they deliver, and their green options.
Hallpack has 20 years of experience and uses recyclable materials, and they also offer custom designs.
Future trends include coatings made from plants and automation in smart factories.
Choosing the right supplier for food packaging requires more than comparing prices. You need a partner who understands the strict rules around packaging and food-safe use. Two critical areas demand your attention: certifications and material performance. Let's break down what matters most.
Food-grade paper tubes must meet rigorous safety standards before they touch your products. In the United States, the FDA regulates food contact materials under 21 CFR Part 176. This regulation uses a positive-list approach, meaning only approved substances can contact food. The EU follows a different path with Regulation 10/2011 for plastic coatings, while paper products fall under national laws like Germany's BfR recommendations.
Aspect | FDA (21 CFR Part 176) | EU 10/2011 & related |
|---|---|---|
Regulatory structure | Positive-list approach (CFR listing, FCN, TOR exemption) | Harmonized measures for plastics; paper covered by national laws (e.g., BfR) |
Migration limits | Extraction limits for specific polymer components | OML of 60 mg/dm²; SMLs for individual substances |
Testing methodology | FDA guidance specifies simulants and conditions | EU 10/2011 specifies simulants (A, D1, D2) and EN standards |
Declaration format | No mandated format; industry practice | Declarations of Compliance per Article 15 of Regulation 1935/2004 |
Traceability | No comparable requirement; GMP and supplier documentation | Article 17 requires traceability through all stages |
You should always request documentation proving compliance with these standards. A reputable supplier will share test results and declarations without hesitation. This verification step protects your brand and your customers.
The barrier coating on your paper tube determines how well it protects food from moisture and grease. Two common options dominate the market: PE (polyethylene) and PLA (polylactic acid). Each offers distinct advantages depending on your product needs.
Coating Technology | Moisture Barrier | Grease Barrier | Key Features |
|---|---|---|---|
PE (Polyethylene) Extrusion | Ultimate water and moisture barrier | Not specifically rated; excellent heat sealability aids in grease containment | FDA compliant; requires specialized recycling facilities |
PLA (Polylactic Acid) Coating | Excellent moisture barrier | Excellent grease barrier | PFAS-free, FDA compliant, industrially compostable |
The manufacturer explicitly states that PE coating offers better moisture protection than PLA coating, while also noting PE's additional advantages in heat resistance and cost-effectiveness.
For sustainable packaging, PLA provides an eco-friendly alternative that breaks down in industrial composting facilities. However, if your product faces high humidity or extended storage, PE might serve you better despite its recycling challenges. Many paper tube manufacturers now offer both options, letting you choose based on your specific requirements.
Hallpack's products meet these rigorous standards, using recyclable construction and eco-friendly materials throughout their manufacturing process. Their precision engineering ensures consistent barrier performance across every batch. When evaluating suppliers, always request samples and test them under your actual storage conditions. This hands-on approach reveals how well the packaging performs in real-world scenarios. Look for fda-compliant liners that match your product's fat content and moisture sensitivity. The right combination of certification and material quality ensures your food arrives fresh and safe.
The American market has many good choices for food-grade paper tube packaging. Each supplier has its own strengths. Some have huge production capacity. Others offer special customization. Knowing these differences helps you pick the right partner.
Sonoco is one of the biggest packaging companies in the world. It works on many continents. Its size means it can handle very large orders with steady quality. National brands that need millions of tubes each year often choose Sonoco. They have special facilities for food-grade packaging. Their production lines meet strict hygiene standards. Their engineering team works closely with clients. They design tubes that survive shipping and keep food fresh. For companies with high-volume needs, Sonoco’s reliability and infrastructure make them a solid choice. They also invest a lot in research. They test new barrier materials and coating technologies. This focus on innovation keeps them ahead in the industry. If you need large quantities with tight deadlines, Sonoco’s production capacity can deliver.
Custom Paper Tubes takes a different approach. They focus on sustainability and flexibility. They specialize in smaller runs and custom designs. This makes them great for boutique food brands and startups. Their commitment to eco-friendly materials runs deep in their product line. Here’s what you can expect from their food-grade packaging:
Cardboard tube and end cap made from post-consumer materials
Food grade liner for product safety
Kraft paper cap with slip cover style for easy opening
Soy-based inks for labeling that reduce environmental impact
Their kraft paper cap tubes use recyclable paper. Most of it comes from recycled packaging materials. This approach cuts waste without losing durability. Custom Paper Tubes also helps you create packaging that shows your brand identity. They work with you on printing, sizing, and structural design. This helps your packaging stand out on store shelves. For businesses that care about sustainable packaging, this supplier offers a mix of environmental responsibility and design flexibility.
Beyond these two leaders, several other US suppliers deserve attention. Conitex Sonoco, a joint venture, makes specialty paper tubes for food packaging. They offer advanced barrier solutions for tough products. All Paper Tube Co. provides reliable mid-volume production with quick turnaround times. They serve regional food manufacturers across the country. Valk Industries and Western Container Corp round out the list as notable regional suppliers. Each offers competitive pricing and dependable service for local businesses. These companies together represent the best cardboard tube manufacturer options in the US market.
When evaluating these suppliers, think about your production volume, customization needs, and sustainability goals. Ask for samples from at least three candidates. Test them under your actual storage conditions. Check their certifications, including FDA-compliant liners that match your product’s fat content and moisture sensitivity. The right paper tube manufacturers will provide documentation without hesitation. They will work with you to refine their packaging for your specific use. Remember that the cheapest option rarely gives the best long-term value. This is especially true when packaging and retail branding directly affect how customers see your product. Take time to compare quotes, lead times, and material quality before you decide.
Europe leads the charge in circular economy practices for packaging. Strict EU regulations push manufacturers toward recyclable materials and transparent supply chains. When you search for top-rated suppliers for specialty paper tubes used in food packaging, European companies often appear at the top. Their commitment to sustainability pairs with technical precision. Here are two standout manufacturers worth your attention.
Albert Bichler GmbH operates from Austria, serving the premium packaging sector. This company focuses on luxury goods, cosmetics, and pharmaceutical packaging. Their reputation for quality makes them a trusted name across the DACH region and broader European markets. They position themselves among the top 10 paper tube packaging companies in Europe.
What sets Albert Bichler apart is their dedication to sustainable packaging. They use responsibly sourced paper and eco-friendly adhesives throughout their production process. Their manufacturing facility follows strict environmental standards. This approach appeals to brands that want premium aesthetics without compromising their green credentials. If your product needs an upscale presentation, this supplier delivers refined finishes and precise printing.
Their compliance with EU food contact regulations is thorough. They provide full documentation for every batch. You can request migration test results and material declarations before placing an order. This transparency builds trust and simplifies your own compliance work. For food brands targeting the European market, Albert Bichler offers a reliable partnership.
Paper Tubes and Cores Ltd operates from the United Kingdom. They serve both UK brands and the broader European market. Their product range includes industrial cores and consumer tubes. This versatility makes them a flexible partner for various packaging needs. They also rank among the top 10 paper tube packaging companies in Europe.
Their strength lies in advanced barrier technology. They develop coatings that protect food from moisture and grease migration. These barriers keep snacks fresh and prevent oil stains from ruining your packaging appearance. Their engineering team works closely with clients to match barrier properties to specific food types. Whether you package dry goods or oily products, they tailor the solution.
UK-based production gives you domestic supply chain control. Shorter shipping distances mean faster delivery times. This advantage matters when you need quick turnaround for seasonal products. Their customer service team responds quickly to inquiries. They also offer competitive minimum order quantities compared to larger US manufacturers. For mid-sized food brands, this flexibility proves valuable.
Company | Country | Market Focus | Relevance |
|---|---|---|---|
Albert Bichler GmbH | Austria | Premium European packaging (luxury, cosmetics, pharma) | Strong access to DACH region and broader European markets |
Paper Tubes and Cores Ltd | United Kingdom | UK and broader European market (industrial cores, consumer tubes) | Serves UK brands with domestic supply chain control |
When comparing European suppliers to their US counterparts, consider lead times and minimum order quantities. European manufacturers typically offer smaller MOQs. This flexibility suits startups and boutique brands testing new products. US suppliers like Sonoco excel at massive production runs. European paper tube manufacturers focus on customization and sustainability. Shipping costs also differ. If you sell primarily in Europe, choosing a local supplier reduces freight expenses and carbon footprint. If you sell globally, weigh the trade-offs carefully.
The best cardboard tube manufacturer for your business depends on your market reach and volume needs. European suppliers shine in premium packaging and regulatory compliance. Their sustainable packaging practices align with consumer expectations across the continent. Request samples from at least two European candidates. Test their barrier performance under your storage conditions. Verify their certifications match your target markets. This diligence ensures your packaging meets both safety standards and brand promises.
You now have ten strong choices across the US and Europe. Each one has different strengths. To pick the right one, you need to compare them side by side. Focus on three key areas: production capacity, lead times, and sustainability features.
Production capacity varies a lot among these suppliers. Sonoco handles huge orders with ease. European makers like Albert Bichler focus on smaller, premium runs. Your order size decides which partner fits best.
Lead times also differ a lot. Standard custom orders usually take 3-4 weeks for amounts between 500 and 5,000 pieces. Highly customized orders may take longer than that. Ask every supplier about their rush production options before you commit.
Supplier | Region | MOQ | Lead Time | Key Strength |
|---|---|---|---|---|
Sonoco Products Company | US | High | 3-4 weeks | Massive production capacity |
Custom Paper Tubes | US | Low | 3-4 weeks | Eco-friendly customization |
Conitex Sonoco | US | Medium | 3-4 weeks | Specialty food packaging |
All Paper Tube Co. | US | Medium | 2-3 weeks | Quick turnaround |
Valk Industries | US | Low | 2-3 weeks | Regional supply |
Western Container Corp | US | Medium | 3-4 weeks | Regional supply |
Albert Bichler GmbH | Austria | Low | 3-4 weeks | Premium finishes |
Paper Tubes and Cores Ltd | UK | Low | 2-3 weeks | Advanced barrier coatings |
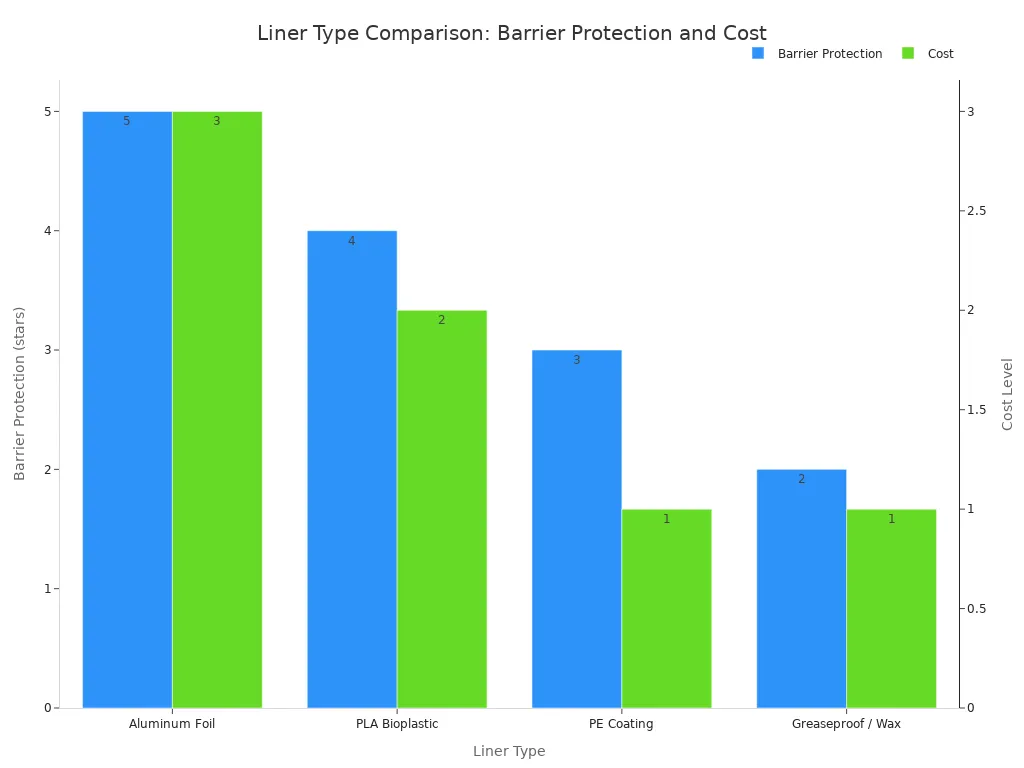
Balancing budget with environmental care takes careful thought. Paper tube packaging costs less than many other options while staying eco-friendly. This mix makes it attractive for food brands of all sizes.
Your liner choice directly affects both cost and sustainability. Aluminum foil offers the strongest barrier but costs more and cannot compost. PLA bioplastic liners give great protection and compost in industrial settings. PE coating costs the least but usually cannot compost. Greaseproof paper offers a budget-friendly option for oily products.
Hallpack shows that fair pricing and sustainable packaging can work together. They use recyclable materials and eco-friendly production methods without raising costs. This approach makes them a strong choice among top-rated suppliers for specialty paper tubes used in food packaging.
When you look at quotes from different paper tube manufacturers, use this checklist:
Request material certifications and confirm quality control processes
Ask about dimensional tolerances and adhesive bond strength
Verify recyclable materials and sustainable sourcing (FSC, SFI)
Confirm custom sizes and printing options match your brand needs
Compare MOQ costs for smaller runs versus bulk orders
Test samples under your actual storage conditions
The best cardboard tube manufacturer for your business balances all these factors. Consider your volume needs, sustainability goals, and budget constraints together. Request samples from at least three candidates before making your final decision.
This guide talks about US and European suppliers. But one Chinese company is worth your time. Hallpack is based in Heshan City, Guangdong. They work in many industries around the world. With over 20 years of experience, they are a top choice for specialty paper tubes used in food packaging. They offer good prices and quality that meets international rules.
Hallpack started more than 20 years ago. Their factory uses advanced machines for every step of making tubes. Precision rolling, automated cutting, and real-time checks make sure each tube is exactly right. Their sealing machines add extra reliability, so every batch has no defects.
"We have over 20 years of experience, making us the leading manufacturer in the industry."
They make packaging for many products. You can find solutions for food and drinks, cosmetics, supplements, gifts, and online shipping. This variety means they know the rules for different industries. They are committed to eco-friendly packaging. They use recyclable materials and green processes without losing strength.
Hallpack is great at OEM/ODM partnerships. You bring your design idea, and their team handles everything from the first model to final delivery. Their customization options give you full control over your packaging:
Customization Aspect | Available Options |
|---|---|
Sizes | 8 standard sizes from 50 ml to 750 ml, with dimensions from D55×H50 mm to D153×H70 mm; you can also ask for custom sizes |
Prints | Full 360° print area; supports CMYK, Pantone, foil stamping, and embossing; the top lid can match or contrast the body |
Coatings/Outer Layer | Premium smooth coated paper; choices include coated, textured, metallic, or kraft finishes |
Their global delivery network makes sure your custom tubes arrive safely anywhere in the world. Certified workers handle loading, and strong boxes protect your products during shipping. This care makes them a strong choice when you compare paper tube makers.
Hallpack shows that eco-friendly materials and good prices can go together. They are a top cardboard tube maker because of steady quality and helpful service. When you need packaging that shows your brand, they deliver solutions that work worldwide.
The packaging world changes fast. What works today may feel old tomorrow. Smart brands watch new trends closely. They want partners who create new ideas, not just suppliers who take orders. The top 10 cardboard tube manufacturers for 2026 will lead with new materials and smarter factories. Knowing these changes helps you pick the right partner.
Plant-based coatings are changing what paper tubes can do. These new materials come from plants, not oil. They break down naturally after use. This change matters for food brands that want packaging that can be reused or composted.
Here are the key changes to watch:
Bio-Based and Compostable Coatings: Makers now use polylactic acid (PLA), polyhydroxyalkanoates (PHA), starches, and plant-based polymers. Strong compostable coatings now match the oxygen barrier of synthetic polymers. The main goal is improving moisture barrier and heat resistance for tough jobs.
Water-Dispersible Barrier Layers: Special polymer coatings dissolve in water. This stops contamination during recycling. These coatings let paper packages recycle without plastic lining problems. They replace thick multi-layers or foil with thin coatings that come off easily.
Market studies show other useful materials:
Chitosan forms clear, flexible films that create a full barrier on paper surfaces.
Starch-based coatings are recyclable and compostable, good for eco-friendly food packaging.
Nanotechnology and biotechnology allow high-performance coatings with natural materials.
These new ideas mean your packaging can protect food and still break down after use. When you check top-rated suppliers for specialty paper tubes used in food packaging, ask about their coating choices. The best cardboard tube manufacturer will offer many eco-friendly options.
Smart factories use artificial intelligence and the Internet of Things. These tools check quality in real time. Sensors measure diameter tolerance and load-bearing performance during production. AI spots flaws right away. This cuts waste and makes sure every tube meets your needs.
Automation also makes production faster. Machines work all day with steady precision. This means quicker delivery times for your orders. Paper tube manufacturers who use smart manufacturing give higher quality at fair prices.
These trends change how you pick suppliers. You need partners who put money into research and development. Forward-thinking companies like hallpack already use precision engineering and real-time quality inspection systems. Their automated processes ensure defect-free products batch after batch.
The top 10 cardboard tube manufacturers for 2026 will mix sustainable materials with smart production. Pick a partner who uses both. Your packaging will stay fresh, look good, and help the planet.
Your best supplier depends on your priorities. Big brands need scale like Sonoco. Small firms want custom designs from Europe. Eco-focused businesses should check hallpack's recyclable options.
Always check certifications before you commit. Request FDA or EU documents. Test samples in your storage conditions. This care prevents costly mistakes.
Hallpack is worth considering for custom designs. Their 20+ years of experience means reliable quality. They use eco-friendly materials and fair prices. Their global network delivers to your facility safely.
Ready to improve your packaging? Contact hallpack now to start working together. Their team will help you at every step, from design to delivery.
You need FDA approval for selling in the US. For Europe, check that the supplier follows Regulation 10/2011. Ask for migration test results and Declarations of Compliance. A reliable supplier will share these papers without delay. Check them carefully before you place any order.
PE coating keeps moisture out better and handles heat well. PLA coating blocks grease and breaks down in industrial compost. Your product's storage conditions decide which one to pick. If humidity is high, PE is the better option. Brands that care about the environment often choose PLA, even though it does not block moisture as well.
European suppliers usually have lower minimum orders than US companies. Custom Paper Tubes and hallpack can handle smaller batches. Sonoco needs bigger orders because of how their factories run. Ask each supplier about their minimum order rules before you request a price quote.
Yes. Hallpack meets FDA and EU rules for food contact. Their careful engineering and real-time quality checks keep results steady. They use recyclable materials and green production methods. With over 20 years of experience, they are a dependable OEM/ODM partner.
Standard custom orders take 3-4 weeks for amounts between 500 and 5,000 pieces. Designs that need extra customization may take longer. European suppliers deliver faster to customers in their area. Hallpack's worldwide shipping network makes sure your tubes arrive safely anywhere.


 English